Hey everyone, I’m gonna cut right to the chase here—if you’re reading this, odds are you work with special structure molds and have been banging your head against the wall trying to get parts to release cleanly, right? I’ve been in this game for 12 years, running a small special structure mold supply business, and I’ve seen every kind of release fail: parts tearing off undercuts, plastic staying stuck in core pins, even super weird “ghosting” marks that make custom parts get rejected. Most of the time, it’s not that your mold is junk—it’s that you’re missing small, structure-specific tricks that generic mold guides don’t tell you. Let me walk you through the stuff that actually works, no fluff, just what we test every single day for clients who come to us with wonky, complex molds (think undercuts with angles steeper than 15 degrees, internal cores, or thin, weirdly shaped sections that regular molds never see). Special Structure Mold
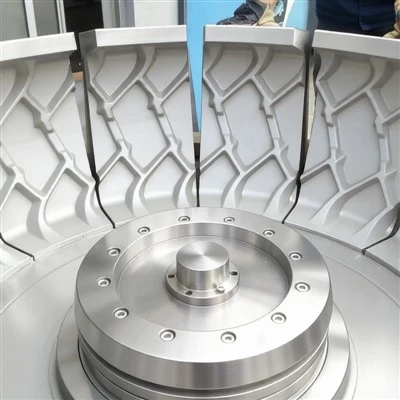
First off, let’s get one thing straight: special structure molds aren’t your basic milk jug molds. They have moving parts that regular molds don’t—side actions, split cores, lifters that tuck into tight spots, all stuff that makes release way harder because there’s more surface area touching plastic, and those surfaces are often uneven or in places you can’t easily reach. I used to think just spraying more mold release was the answer, but I learned fast that that’s a band-aid that makes things worse: too much release builds up gunk, makes parts slippery and hard to trim, and can cause inconsistencies in surface finish. The real fix is matching your release method to the specific structure of your mold, not just grabbing the same aerosol you’ve used for years.
Let’s start with the most common headache for us: undercut features. These are the parts that stick out or indent, like a screw thread on a custom widget or a tab that locks two parts together. For regular straight walls, draft angles (that tiny slant you put on mold cavities) are enough, but undercuts? If your draft is less than 10 degrees, even a tiny bit of shrinkage on the plastic will clamp the part so tight it won’t come off. Here’s what we do when we’re building a special structure mold for a client with undercuts: we add “ejector pins” right at the thickest point of the undercut, not just the edge. Wait, no—wait, don’t just add pins where it’s easy. We mill tiny, shallow reliefs (like 0.005 inches, max) into the side action walls right at the undercut’s sharp corner. That gives the plastic a tiny gap to pull away from the mold before the ejector even hits. We also test draft angles with the actual plastic the client’s using, not just generic numbers. If it’s a rigid plastic like ABS, we bump draft to 12 degrees for deep undercuts; if it’s a softer TPU, we go up to 14 degrees because soft plastic shrinks more and sticks harder. I had a client last month who was rejecting 20% of parts because their existing mold only had 7 degrees of draft on a complex side undercut—we re-milled that draft, added two small reliefs, and their reject rate dropped to less than 1%. No new mold, just adjusting the structure for release.
Next up: internal cores. These are the ones that run through the middle of a part, like a pipe fitting or a hollow custom bracket. The problem here is that the plastic is shrinking onto both the outer cavity and the inner core, so you have two surfaces pulling at once. Most guys just use a lot of spray release on the core, but that’s a disaster because you can’t evenly coat a tiny, long core with an aerosol—you get thick spots that cause flash or thin spots that stick. We use two things here: first, “polishing” the core to a super smooth finish, not the standard 16 microinch Ra (that’s the surface roughness number, for anyone who’s curious). For internal cores, we go to 8 microinch Ra, and we finish it with a diamond-tipped buff, not sandpaper. Smooth surface means less friction, full stop. Second, we use a “dry film lubricant” applied to the core when it’s built, not sprayed on every cycle. Dry film is like a super thin, hard wax that bonds to the metal, doesn’t wash off with plastic heat, and lasts for hundreds of cycles. We tested it once on a long, 6-inch internal core for a medical component client—they were spraying release every 50 cycles and still had sticking. We applied the dry film, and they only needed a touch-up every 500 cycles, and their parts released 100% without tearing. Pro tip here: don’t use PTFE-based dry film for cores that see high heat (over 200°F)—it melts and leaves a mess. Go with a molybdenum disulfide dry film, it’s way more heat-resistant and works better for high-temp plastics like nylon.
Wait, let’s talk about lifters too—those little moving parts that pop up to form undercuts when the mold opens, then go back down so the part can eject. Lifters are such a hidden release killer because their contact points are tiny and often angled. Most people forget to check the gap between the lifter and the main mold body. If the gap is too small (less than 0.002 inches), when the mold heats up and expands, the lifter gets stuck to the cavity wall, and the part comes out with a chunk missing. We set the gap at 0.003 inches, no exceptions, for any lifter on a special structure mold. Also, we add a tiny “lead-in” slope to the top of the lifter that contacts the part—like a 2-degree slope that faces the ejector direction. That way, when the lifter moves up to form the undercut, the plastic slides onto the slope instead of catching on a sharp edge, which means it pulls away cleaner when the lifter retracts. I can’t tell you how many times a client has come to us with “lifters sticking” and that’s the only fix they needed—no new parts, just adjusting that 0.001 inch gap and adding that little slope.
Now, let’s get to the stuff you do between runs, not just when building the mold. Even if your mold is perfect, gunk build-up is gonna ruin release. For special structure molds, the spots you need to clean are the tiny, hard-to-reach places: the gaps between side actions, the ejector pin holes, the reliefs you milled for undercuts. Most guys just spray release and wipe the big surfaces, but the small spots trap leftover plastic and release that hardens, creating bumps that catch parts. We use a dental pick (the tiny ones, not the big mechanic ones) to get into those gaps between runs, and once a week, we do a “deep clean” with isopropyl alcohol and a soft microfiber cloth—no harsh chemicals that can scratch the mold. Also, don’t forget to check your ejector pins! Even a tiny bent pin will push unevenly, making parts stick. We replace ejector pins every 10,000 cycles for special molds, not 50,000 like regular molds, because they work harder on complex parts.
Wait, one big mistake I see all the time: using the wrong mold release product for your plastic. If you’re using a specialty plastic like PEEK or polycarbonate, regular silicone-based release won’t work because those plastics are way more adhesive. For high-performance plastics, we use a water-based release that’s formulated for engineering resins, not the aerosol for polypropylene. Aerosol releases can build up on small, tight structures and cause surface defects that get rejected, while water-based releases vaporize faster and leave less residue. I had a client who was running PEEK parts with a side action mold, using a standard aerosol and getting 15% surface rejects from release build-up. Switched to water-based release, rejected rate dropped to 2%—game. Changer.
Also, let’s talk about mold temperature, because that’s a big one for release too. For special structure molds, especially ones with internal cores or deep undercuts, if the mold is too cold, the plastic shrinks too fast, clamping tight. If it’s too hot, the plastic is soft and sticks more. We set mold temps 5°F lower than what the plastic supplier recommends, and for parts with undercuts, we even cool the core lines a tiny bit more than the cavity lines. The cavity is the outer shape, so cooling it a little slower means it’s still flexible when it pulls away, but the internal core cools faster, so shrinkage happens on the core first, not the cavity. That’s a trick most generic guides don’t mention, and it’s saved so many clients from stuck parts.
Now, let’s get real—if you’re dealing with a special structure mold, you can’t treat it like a standard mold. Generic tips (add more draft, spray release) only get you so far. The key is to build release into the structure of the mold itself, not just add it later. That’s what our team focuses on when we make custom special molds—we don’t just machine the parts, we test every moving feature, every undercut, every core pin for release before we send it to the client. We also work with them on their process, because even the best mold won’t work if they’re running it wrong.
If you’re sick of reject rates, stuck parts, and wasting hours trimming off parts that won’t release, hit us up. We don’t do one-size-fits-all solutions—we look at your specific mold, your plastic, your part design, and tweak the structure and process to get that release you need, no guesswork. Whether you’ve got an existing mold that’s acting up and need a quick fix, or you’re designing a new special structure mold and want to nail release from day one, we’re here to help.
Wait, before I wrap up, let me leave you with two quick checks you can do right now on your own mold, no fancy tools needed. First: take a flashlight and look at the gaps between your side actions and the main mold. If you can’t get a thin business card in there, the gap is too small—fix that and you’ll cut down on lifter sticking. Second: check the draft on your deepest undercut. If it’s less than 10 degrees, add at least 2 more degrees and you’ll probably see a difference.
Oh, and one more thing—don’t over-polish areas that need a little grip. I’ve seen guys polish the entire mold to mirror finish, and that actually makes parts stick more sometimes, because there’s no tiny micro-roughness to break the plastic’s surface tension. Only polish the contact areas that slide—leave the reliefs and draft areas with a little texture for grip.
Alright, that’s the stuff that’s actually worked for us over the years, not the textbook stuff. If you’re ready to stop fighting with stuck parts, reach out to talk through your specific mold issues. No sales pitch garbage, just real answers from guys who work with special structure molds every single day.
Two Piece Mold References:
- Mold Making & Design, "Undercut Release Optimization for Complex Injection Molds", 2022
- Society of Plastics Engineers, "Lubrication Strategies for Internal Core Mold Features", 2021
- Plastics Technology, "Mold Temperature Tuning for Release of High-Shrink Engineering Resins", 2023
Anhui Varon Mould Co., Ltd.
We are one of the most professional special structure mold manufacturers and suppliers in China, also support customized service. We warmly welcome you to wholesale premium special structure mold made in China here from our factory. If you have any enquiry about cooperation, please feel free to email us.
Address: Anhui Province, Ningguo City, Economic and Technological Development Zone, Heli Industrial Park, Dongcheng Avenue
E-mail: admin@varonmould.com.cn
WebSite: https://www.wanlongmold.com/
